Call Us Today!
 Alibaba.shop
0
CART
You have no items in your shopping cart
company
Company
Our customers can count on us because we offer them safety, continuity, and transparency.
products
Products
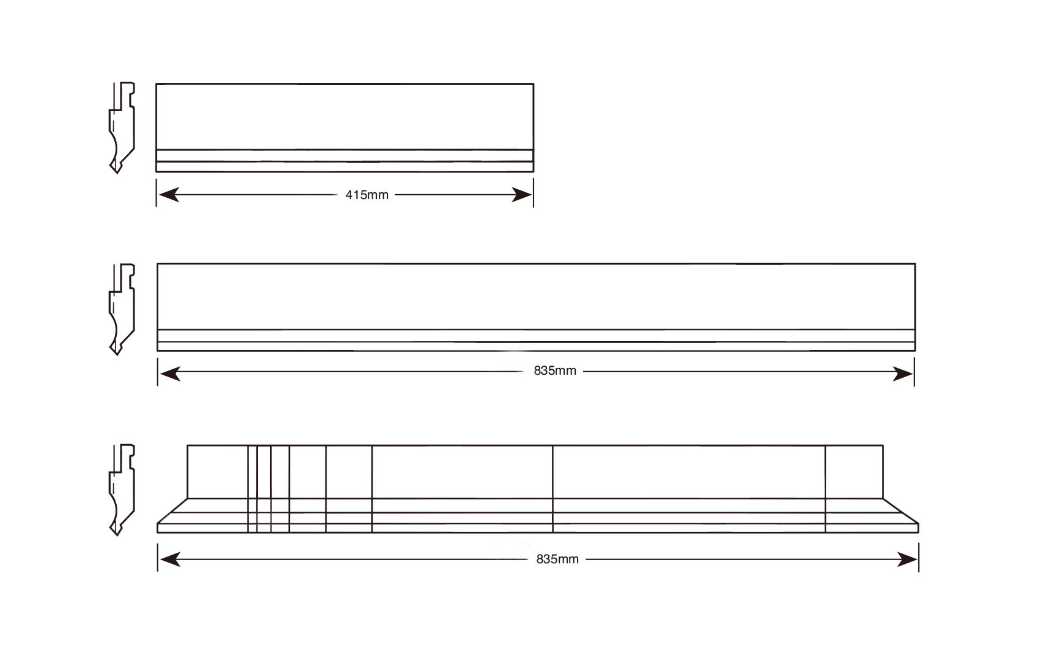
A wide range of innovative solutions from press brake tooling, clamping system and crowing table, can be found within the FABMAX products range.
service
Service
We provide personal and specialized consultation to ensure an optimal production solution to suit the needs of any business.
resources
Resources
contact
Contact
Get in touch to request a call back from one of our Engineers about your project.