Call Us Today!

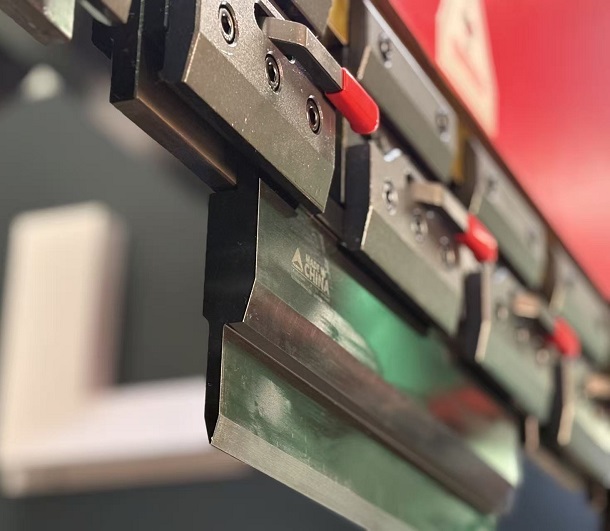
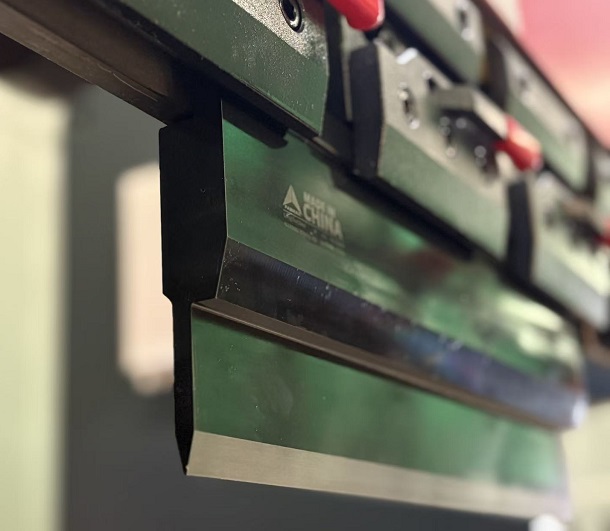
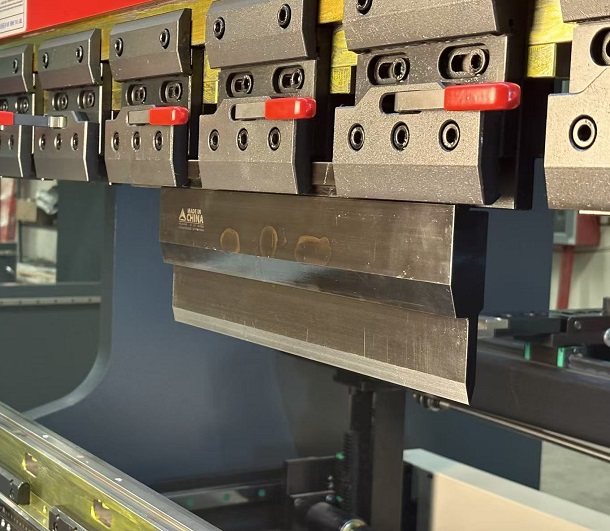
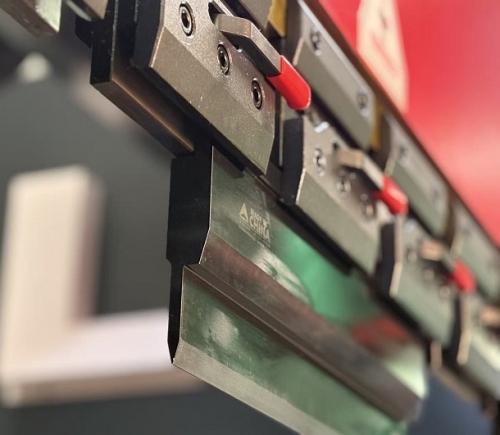
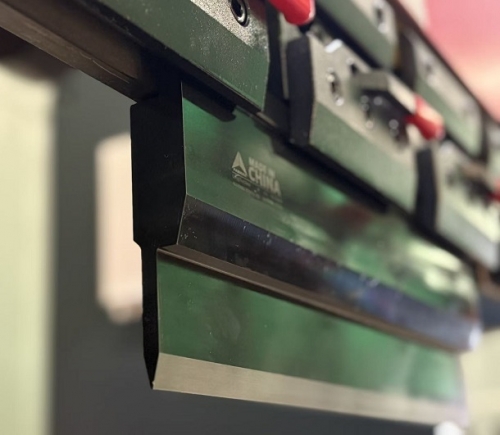
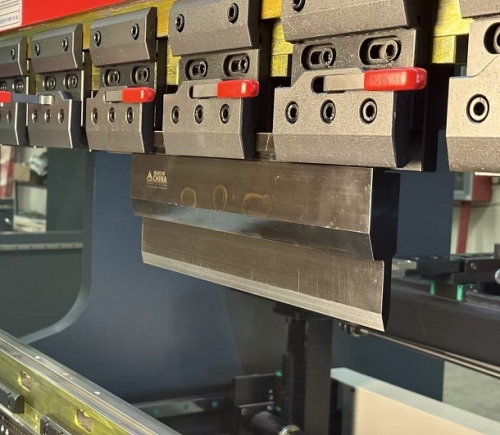
FMHP.128.24°.12

$320.00Excl.tax Excl. Shipping costs
* Length(mm)
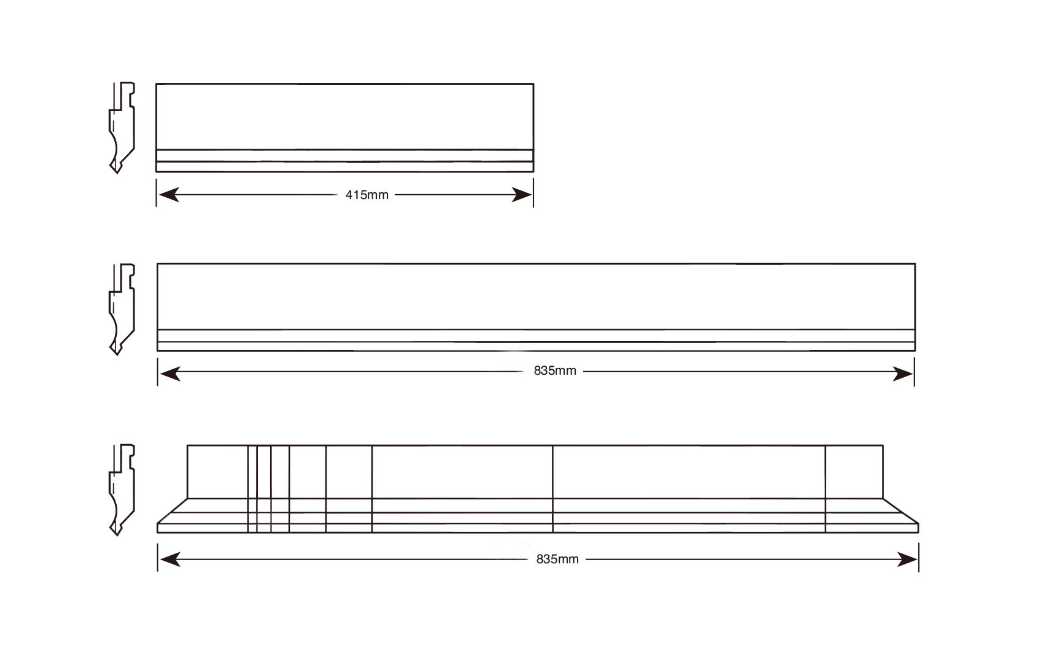
L=835mm L=415mm Sec.
TEAMS
Dedicated service teams.
KNOW-HOW
More than 25 years of experience
QUALITY
Outstanding quality
SERVICE
24-hour quick response
  • Information
  • FABMAX-System Amada

    Angle: 24°
    Radius:R 0.6 mm
    Height:158 mm
    Load:Max T/m=80.
    Material:42CrMo, 650 - 800 N/mm

    Punch FEature
    1. Most tools can be easily loaded by a single operator.
    2. Easy to store.
    3. All sectionalised tools come pre-cut in nine different pieces.
    4. Most sectionalised punches include two ear pieces (horns).
    5. Punches are induction hardened, to 45-50 HRC but 55-60HRC is available for every punch in the tooling line.
    6. Special Tooling available.

    PUNCH SECTION LENGTHS: 100mm LEFT EAR / 100mm RIGHT EAR / 10mm / 15mm / 20mm / 40mm / 50mm / 200mm / 300mm Note: Special lengths are available at additional cost, just select the standard length and ask us to cut to your requirements.
  • Air Bending Force
  •  
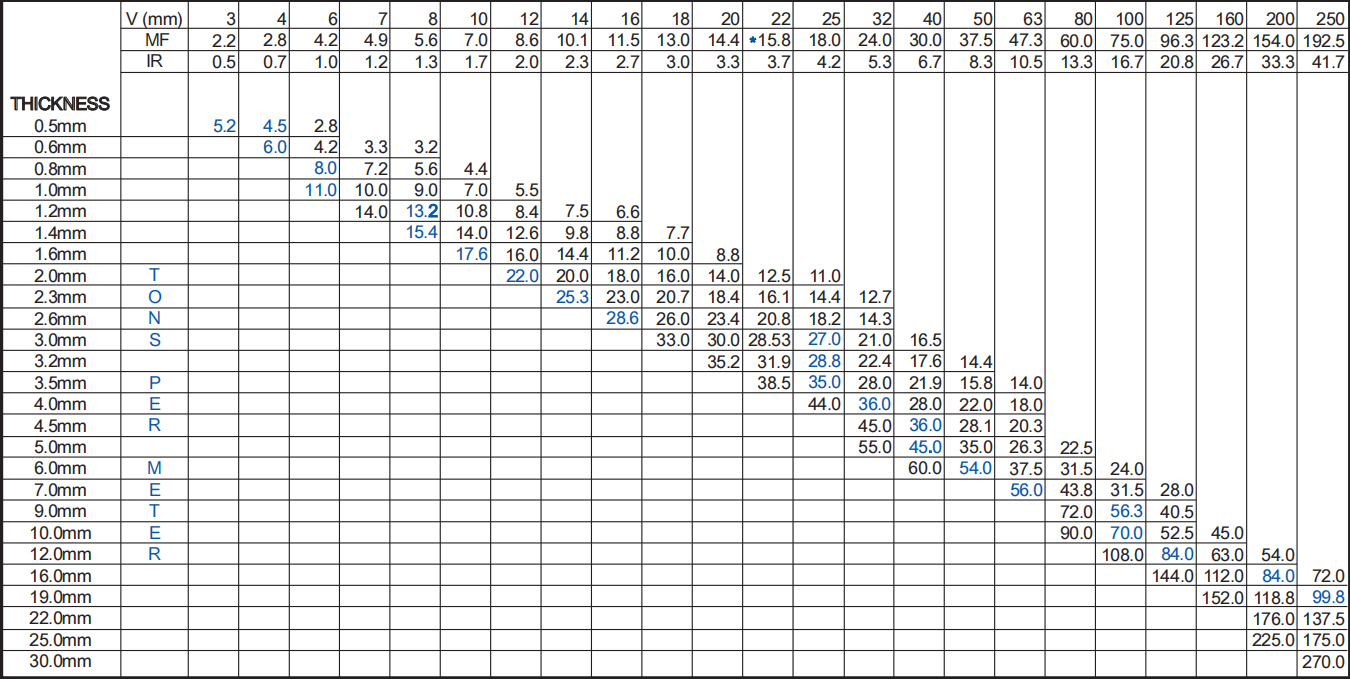
    Air bending force
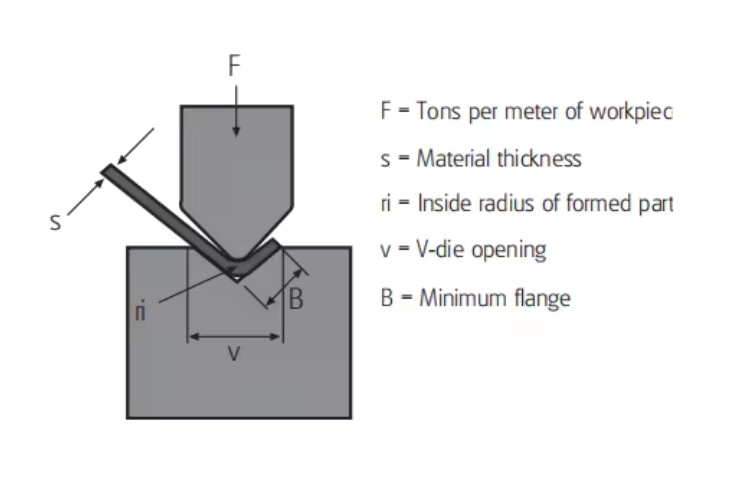
    Required press force at 90° air bending, force in ton/mtr.

    The charts below give the appropriate tonnage to air bend mild steel.

    Bending force for other metals:
    Soft aluminium Tons per unit length x 50%
    Aluminium alloys heat treated Tons per unit length x 100% 
    Stainless Tons per unit length x 150%


  • Items
  • Order:
     
    Minimum order is $20.00.
     
     
    Special Orders:
     
    All special orders are non-cancelable, non-returnable, and non-refundable. 
     
     
    Payment Terms:
     
    Terms are net 10 days. Catalog prices are subject to change without notice.
     
     
    Freight:
     
    Orders are shipped F.O.B. from our manufacturing facility. (International Shipments are Incoterms: Ex Works).
     
     
    Order Cancellation:
     
    In the event an order is cancelled, an additional charge will be assessed to cover the cost of labor and material.
     
     
    Returned Material:
     
    A handling/restocking fee will be applied to all products returned for credit. A return authorization number and shipping instructions must be obtained in advance before an item can be returned.
     
    Claims:
     
    All claims or product shortages must be made within 30 days of the invoice date.
  • Description
  • Crucial for Achieving a Zero-Radius Hem
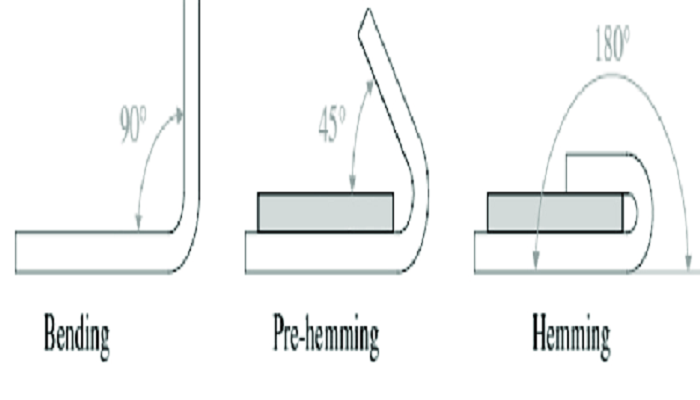
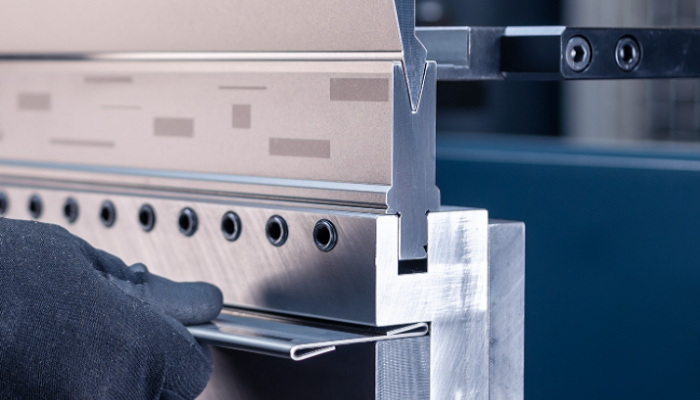
    The final stage of the hemming process relies on the flattening bending punch to apply immense, uniform pressure across the pre-bent material. The design of the Hem Die must ensure the punch achieves perfect parallelism and alignment with the lower die surface to guarantee a true zero-radius hem. Any misalignment during this high-tonnage flattening bending stroke can lead to uneven compression, resulting in a substandard edge finish or potential tooling wear. This precise tool alignment is key to maximizing part accuracy.
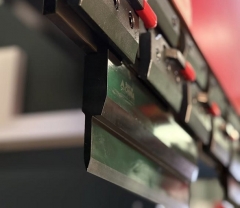
    Hemming tools flattening die press brake tools for sales
    Optimizing Material Flow Before Final Flattening
    The success of the Flattening Tool is directly dependent on the initial acute bend angle. This pre-bend angle (typically between 25° and 35°) must be carefully selected and formed using a dedicated acute angle punch and die set. The angle determines how smoothly the material flows into the Hem Die before the final flattening bending stroke. Incorrect pre-bending can lead to material cracking or an inability to achieve full closure, compromising the final product's structural integrity.
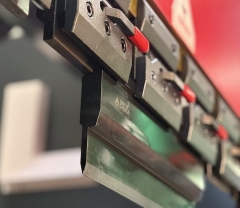
    Hemming tools flattening die press brake tools for sales