Call Us Today!

FMHD.80.12

$350.00Excl.tax Excl. Shipping costs
* Length(mm)
L=835mm L=415mm Sec.
TEAMS
Dedicated service teams.
KNOW-HOW
More than 25 years of experience
QUALITY
Outstanding quality
SERVICE
24-hour quick response
  • Information
  • FABMAX-System Amada

    Angle: 60°
    V-opening: 12mm
    Height:80 mm
    Load:Max T/m=50.
    Material:42CrMo, 650 - 800 N/mm

    Die Feature
    Single V tooling and double V tooling has only one or two tooling grooves, which is very common in CNC press brake and has high precision. Multi-V lower toolings are mostly square toolings with multiple tooling grooves on four surfaces of different sizes. The advantage is that there are many tooling grooves and it can adapt to the bending of various thick plates.

    DIE SECTION LENGTHS:100mm / 100mm / 10mm / 15mm / 20mm / 40mm / 50mm / 200mm / 300mm Note: Special lengths are available at additional cost, just select the standard length and ask us to cut to your requirements.
  • Air Bending Force
  •  
    Air bending force
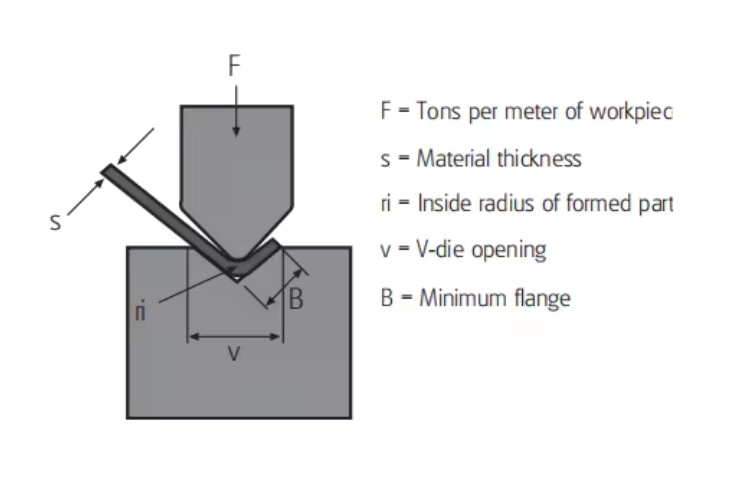
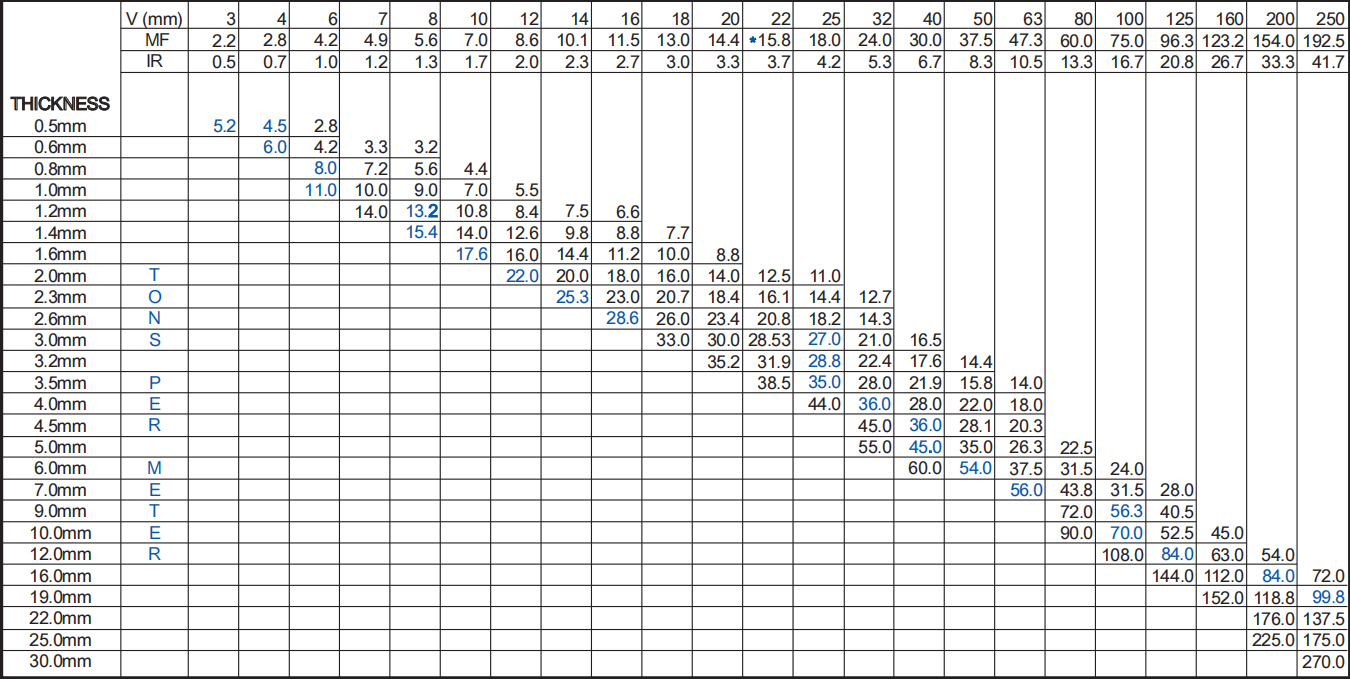
    Required press force at 90° air bending, force in ton/mtr.

    The charts below give the appropriate tonnage to air bend mild steel.

    Bending force for other metals:
    Soft aluminium Tons per unit length x 50%
    Aluminium alloys heat treated Tons per unit length x 100% 
    Stainless Tons per unit length x 150%


  • Items
  • Order:
     
    Minimum order is $20.00.
     
     
    Special Orders:
     
    All special orders are non-cancelable, non-returnable, and non-refundable. 
     
     
    Payment Terms:
     
    Terms are net 10 days. Catalog prices are subject to change without notice.
     
     
    Freight:
     
    Orders are shipped F.O.B. from our manufacturing facility. (International Shipments are Incoterms: Ex Works).
     
     
    Order Cancellation:
     
    In the event an order is cancelled, an additional charge will be assessed to cover the cost of labor and material.
     
     
    Returned Material:
     
    A handling/restocking fee will be applied to all products returned for credit. A return authorization number and shipping instructions must be obtained in advance before an item can be returned.
     
    Claims:
     
    All claims or product shortages must be made within 30 days of the invoice date.
  • Description
  • Cost-Benefit Analysis of the Two-Step Tooling System
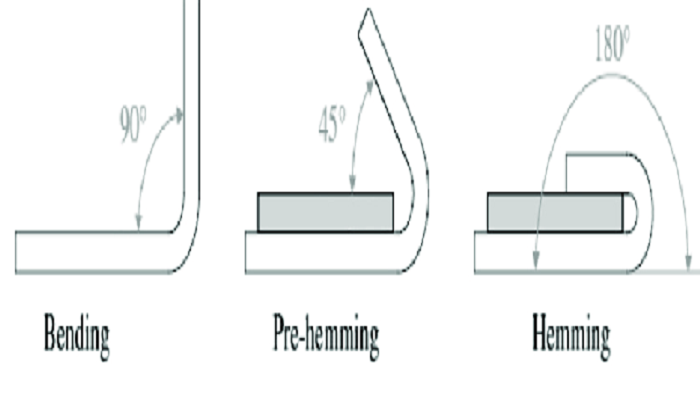
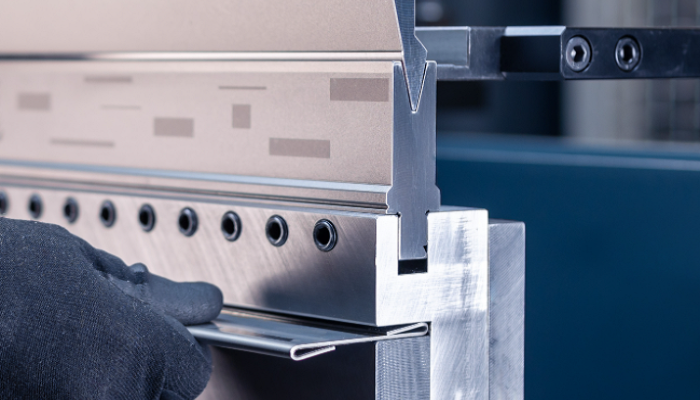
    While the hemming process requires a two-step approach and higher bending tonnage, the resulting safety, stiffness, and aesthetic finish significantly increase the value of the final component. The investment in the dedicated Hemming Tool and the required acute angle punch and V-die set is justified by the elimination of manual finishing work and the superior part repeatability achieved, solidifying its place as a high-value piece of press brake tooling.
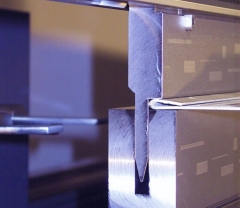
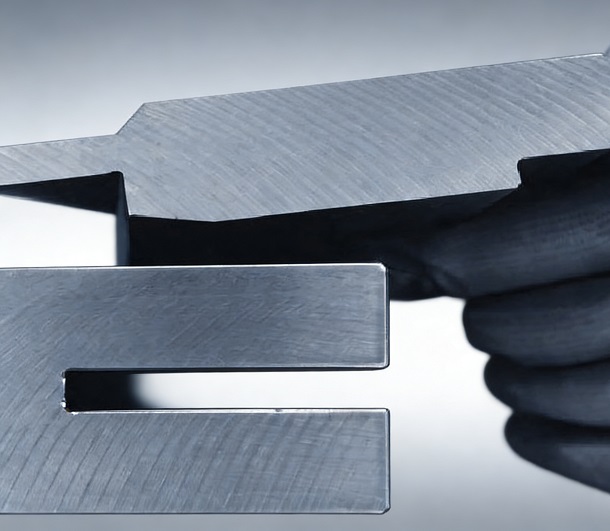
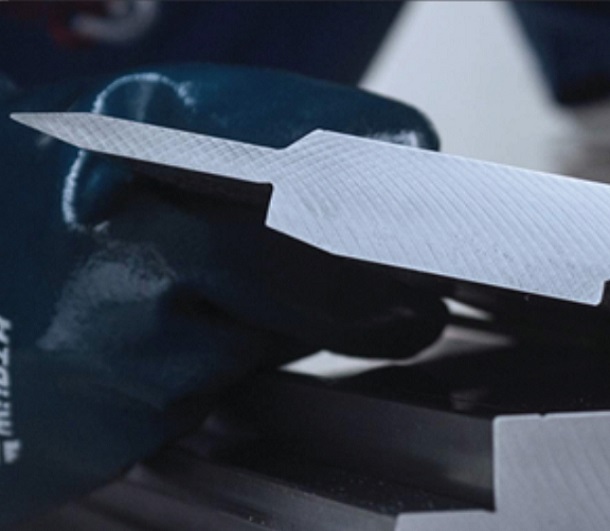
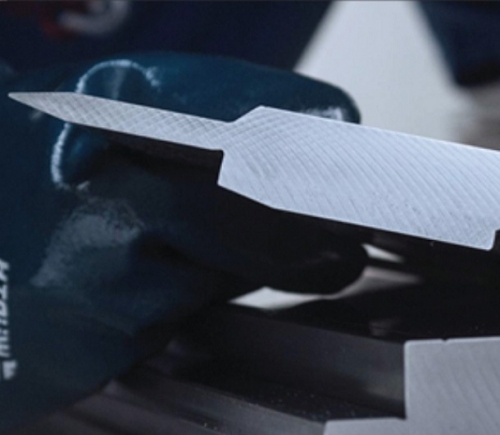
    Hemming Punch Flattening Punch For Sale Press Brake Tooling
    Surface Protection
    For highly sensitive materials (such as polished stainless steel or pre-painted stock), the final flattening bending stroke, despite the smooth surface of the Hemming Die, can still cause cosmetic damage. In these cases, a thin layer of urethane film or non-marking material is often placed between the workpiece and the Hemming Tool during the final compression. This technique allows for the full application of required tonnage while preserving the material's flawless surface finish.
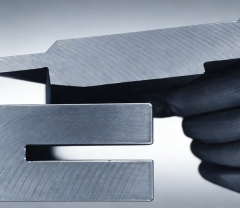
    Hemming Punch Flattening Punch For Sale Press Brake Tooling